The short answer: a nitrogen generator has no single honest “kWh per cubic metre” number without a defined system boundary and operating duty. Divide the electricity used by the compressor, air treatment, generator auxiliaries and any required booster by the usable nitrogen delivered over the same period. State purity, delivery pressure, flow reference conditions and load profile alongside the result.
A generator cabinet may draw little electricity while consuming a substantial flow of compressed air. Quoting only its control-panel power hides the largest upstream load. Conversely, the compressor motor nameplate is not a measurement of what the system consumed during a shift.
What exactly should “energy consumption” measure?
For an installed system, use specific electricity consumption = metered system kWh ÷ usable product nitrogen Nm³. “System” means the equipment actually needed to deliver gas at the agreed point of use. If a customer already owns a compressor, record the nitrogen package’s incremental air demand and a defensible allocation of the compressor electricity; do not call that shared air supply free.
| Record | Why it matters | Where to check |
|---|---|---|
| Compressor input kWh | Usually the main electrical load; rated motor kW is not shift energy | Dedicated power meter or a documented allocation for a shared compressor |
| Dryer, cooling and controls kWh | Auxiliary power and pressure loss belong to the package boundary | Submeters or equipment input logs |
| Booster input kWh, if used | High point-of-use pressure changes the delivered-gas boundary | Booster feeder meter |
| Usable N₂ Nm³ | Off-spec start-up gas, purge and vent should not inflate useful output | Calibrated product meter downstream of acceptance/diversion point |
| Purity, pressure and time window | Two figures are comparable only at the same duty | Analyzer trend, pressure record and synchronized timestamps |
The Compressed Air & Gas Institute (CAGI) performance program uses standardized compressor data sheets and describes compressor-specific power at a stated discharge pressure. That is useful for comparing compressors, but it is not the same as the full nitrogen system’s electricity per usable Nm³. Start by drawing the electrical boundary on the P&ID, then meter it.
A worked calculation: what changes at half output?
Illustrative calculation—not a NITRAISE performance claim or a market benchmark. Suppose a complete package consumes 55 kWh at the compressor and 4 kWh at the dryer and controls during one hour. Its accepted product meter records 100 Nm³ of nitrogen at the specified purity and delivery pressure. The result is (55 + 4) ÷ 100 = 0.59 kWh/Nm³.
Now suppose a different one-hour period produces only 50 usable Nm³ while the entire package still draws 48 kWh. The result is 48 ÷ 50 = 0.96 kWh/Nm³. The 48-kWh figure is an assumption for explaining the arithmetic, not a general part-load rule. A real machine might behave differently depending on its compressor controls, cycling, storage, leaks and shutdown strategy.
This is why a proposal with one “rated-point” figure cannot answer what a two-shift plant will pay to operate. Ask for energy at normal load, minimum sustainable load, peak demand and start-up/standby, with the expected hours at each point. If the application is batch or intermittent, specify the actual production profile rather than an annual-average nitrogen flow.
Why purity changes the answer
PSA and membrane packages separate air rather than manufacture nitrogen. At a given model and inlet condition, a stricter nitrogen purity target can change the amount of compressed air needed per unit of product. Atlas Copco defines the PSA “air factor” as compressed air consumed divided by nitrogen produced and notes its relationship to efficiency in its PSA explanation. The size and direction of a specific project’s energy change must come from matched vendor performance data; the air factor alone does not include compressor and booster electrical efficiency.
Consider a packaging line with an oxygen limit of 0.1%. If procurement requests a more stringent figure without a process reason, the supplier may need more feed air or a different configuration for the same usable flow. The correct decision is not “always choose lower purity.” It is to define the maximum residual oxygen the process can tolerate, the analyzer acceptance point and the consequence of an off-spec event. The nitrogen purity guide explains how to frame that requirement.
Evidence boundary: a product data sheet can demonstrate a model-specific purity/flow trade-off at its stated inlet conditions. It cannot by itself prove the installed system’s electricity per Nm³. Record the selected model’s air consumption, inlet pressure and operating point, then combine those with measured or guaranteed compressor package power.
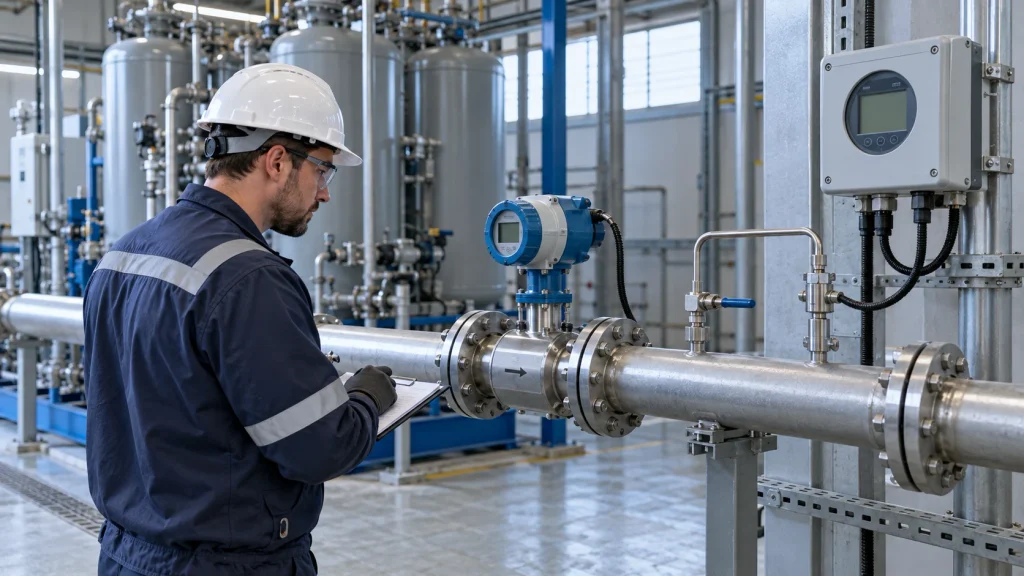
The denominator is delivered, accepted gas—not catalogue flow
Place the product flow meter after the point where start-up gas, analyzer rejects or deliberate venting leave the system. Record the meter’s reference state: “Nm³” needs a stated reference temperature, pressure and dry/wet basis. A catalogue value, an inlet-air reading and a downstream product reading are not interchangeable cubic metres.
Pressure is just as important. If a laser-cutting line needs high-pressure nitrogen at the machine, a low-pressure generator outlet number is incomplete. Include booster electricity and any gas lost through pressure control or distribution. A receiver can smooth a short peak but does not create energy-free nitrogen. Our pressure and booster guide separates generator outlet pressure from point-of-use demand.
A real project shows why the boundary matters
In a supplier-documented food-production project, Atlas Copco describes an 11 kW variable-speed compressor dedicated to a nitrogen generator at Santa Maria. The case is useful because it makes the compressor visible as part of the nitrogen supply decision and discusses choosing the needed purity rather than an arbitrary maximum.
It does not publish a synchronized whole-system kWh and accepted-Nm³ dataset. Therefore 11 kW cannot be converted into a verified kWh/Nm³ figure for that site. This is a supplier-published example, not a NITRAISE project. A specification review should ask for the missing operating hours, product flow, purity and ancillary loads.
Three proposal comparisons that regularly go wrong
| Looks comparable | Hidden mismatch | Make the comparison fair |
|---|---|---|
| “1 kW generator” versus “60 kW nitrogen plant” | One excludes the air compressor; the other may include it | List compressor, dryer, controls, cooling and booster inclusions line by line |
| 100 Nm³/h versus 100 Nm³/h | Purity, outlet pressure, feed-air conditions or volume reference differ | Request both figures at the same accepted specification |
| Two equal full-load kWh/Nm³ values | One plant runs continuously; the other cycles at 30–60% load | Calculate duty-weighted kWh and usable Nm³ over the same shift or week |
The best comparison sheet has a boundary diagram, normal and peak duty points, a part-load curve, guaranteed inlet conditions and the selected compressor’s standardized performance data. Where those are absent, the energy figure is a preliminary estimate.
What to ask vendors before accepting an energy figure
- At which nitrogen purity, usable flow, product pressure and reference conditions is the figure guaranteed?
- Does it include the air compressor, aftercooler, dryer, filters, nitrogen generator controls, cooling and booster?
- What compressed-air flow and inlet pressure does the selected generator need at normal, minimum and peak duty?
- Where are power and product volume metered, and which gas is diverted as off-spec?
- What happens during idling, restart, a temporary flow spike and a production shutdown?
- Which assumptions depend on ambient temperature, altitude, air quality, filter pressure loss or maintenance state?
Send the application, residual-oxygen limit, normal/peak nitrogen demand, required pressure at the use point, operating schedule and available compressed-air data with the RFQ. Our sizing guide covers the flow and duty inputs, and the nitrogen generator RFQ checklist lists the rest of the information suppliers need. Once you have a defensible kWh/Nm³ figure, combine it with local electricity tariff, maintenance, capital and delivery costs in the separate cost guide. This article deliberately does not turn an illustrative energy calculation into a payback promise.
Bottom line: ask suppliers for the same delivered-gas duty and the same equipment boundary. Measure actual input energy and accepted nitrogen over synchronized intervals. Any single “energy consumption” figure without those conditions is a starting question, not a decision-ready answer.
About the author: Henry Xu
Henry Xu is the founder of NITRAISE and a senior industrial equipment engineer with 18 years in nitrogen equipment research, development and production.